Isostatic Pressing for Crack-Free and Delamination-Free Pellets
8月 20, 2026
Pellet cracking, delamination, internal porosity, and uneven density can compromise powder compaction experiments. These problems often arise when conventional uniaxial presses apply pressure from a single direction. Friction between the powder and die wall can create density gradients and residual stress inside the compact. These defects may become more obvious during demolding, sintering, or later material testing.
An automatic laboratory isostatic press addresses these limitations by applying pressure uniformly around the sample. Instead of relying on rigid dies to transfer force along one axis, the system uses a liquid pressure medium to provide multidirectional compression. This approach improves density uniformity, reduces internal stress, and helps produce more consistent green bodies for research and testing.
Why Conventional Pellet Pressing Can Cause Cracking
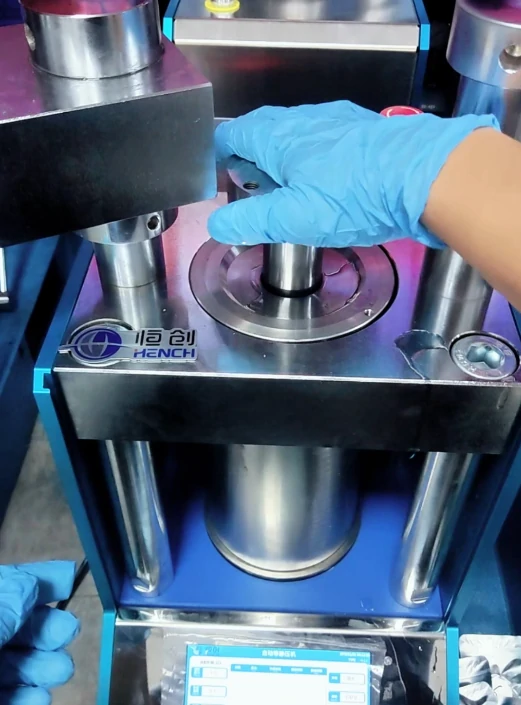
Uniaxial compaction remains widely used for laboratory powder forming. However, its pressure distribution can create challenges when researchers require highly uniform samples.
During conventional pressing, the upper and lower punches transfer force through the powder. At the same time, friction develops between the powder and the die wall. The powder near the punch may compact more effectively than material farther from the pressure source.
This difference can produce a density gradient across the pellet.
Common Defects in Uniaxial Compaction
Several problems may appear during or after pressing:
- Edge-to-core density differences
- Internal porosity
- Residual stress
- Layer separation or delamination
- Edge chipping
- Cracking during demolding
- Warpage during sintering
- Inconsistent test results
The risk becomes more significant when researchers work with powders that have poor flowability or require high compaction pressure.
A compact may appear intact immediately after pressing. However, internal stress can remain within the green body. When the sample leaves the die or undergoes thermal treatment, this stress can trigger cracks or deformation.
For laboratory research, the issue extends beyond sample appearance. Inconsistent density can influence shrinkage, strength, electrical properties, porosity, and microstructure. This can make comparisons between experimental batches less reliable.
How Isostatic Pressing Creates More Uniform Compaction
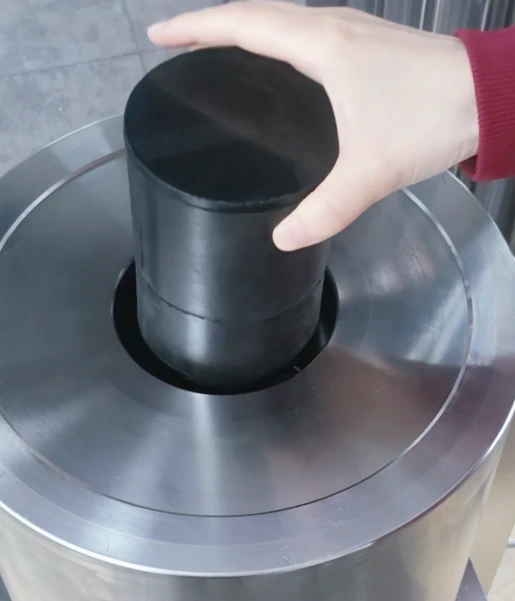
Isostatic pressing uses fluid pressure to compress a powder-filled flexible mold from multiple directions.
The powder is first placed inside a suitable flexible mold. The mold is then sealed and positioned inside a high-pressure chamber. A liquid pressure medium surrounds the mold and transfers pressure uniformly to its external surface.
This process follows the basic principle of pressure transmission through a confined fluid.
Unlike uniaxial pressing, the system does not rely on direct contact between the powder and a rigid die wall to generate the primary compaction force. The flexible mold allows pressure to act around the entire sample.
As a result, the powder experiences more uniform compression throughout its volume.
Uniform Pressure Distribution
The main advantage comes from multidirectional pressure application.
When pressure acts around the sample, the powder particles can rearrange and compact more evenly. The process reduces the localized stress concentrations associated with conventional one-directional pressing.
This can help produce green bodies with:
- より均一な密度
- Lower internal stress
- Reduced porosity variation
- Better structural integrity
- Lower risk of delamination
- ひび割れのリスクを低減
For researchers working with demanding powder systems, these characteristics can make sample preparation more predictable.
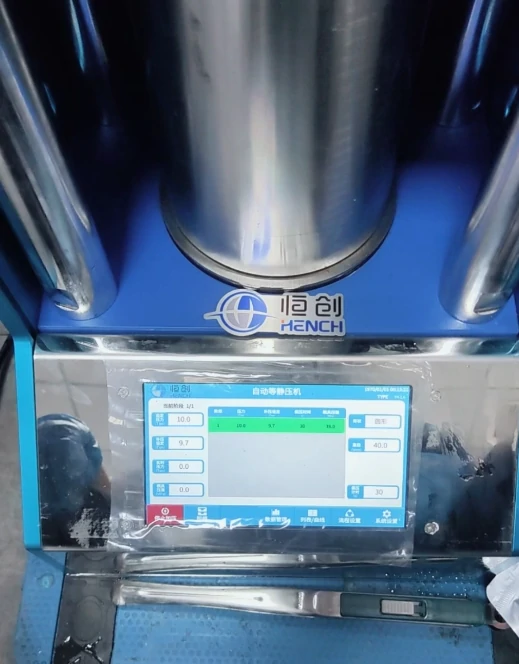
Automatic Control Improves Experimental Repeatability
Pressure uniformity is only one part of a reliable laboratory compaction process. Process control also affects sample quality.
Manual operation can introduce variations during pressurization, pressure holding, and pressure release. Sudden pressure changes may damage fragile green bodies or create differences between experimental batches.
An automatic laboratory isostatic press can address these issues through programmable process control.
Researchers can set key parameters before the cycle begins. Depending on the equipment configuration, these parameters may include:
- Pressurization rate
- Target pressure
- Pressure holding time
- Pressure relief rate
- Process sequence
- Cycle duration
The equipment can then follow the preset sequence with limited manual intervention.
Controlled Pressure Relief
Pressure relief deserves particular attention.
A sudden reduction in pressure can place additional stress on a newly compacted green body. A controlled pressure-release process reduces abrupt changes and supports more consistent sample recovery.
This is particularly useful when researchers need to prepare multiple samples under comparable conditions.
For example, a materials laboratory may need to prepare dozens of ceramic pellets for a sintering study. Using the same programmed pressure cycle for each batch can reduce variations caused by manual operation.
The result is a more standardized experimental workflow.
Suitable for Different Powder Materials and Sample Shapes
Different research fields require different powder systems and sample geometries. A laboratory isostatic press can provide greater flexibility than conventional pellet pressing when sample shape or material behavior becomes more demanding.
Typical applications may include:
| 素材 | Typical Research Application | Key Forming Requirement |
|---|---|---|
| Advanced ceramics | Sintering and mechanical testing | Uniform green density |
| 金属粉末 | Powder metallurgy research | Consistent compaction |
| Electrode materials | Energy material research | Controlled sample structure |
| Magnetic materials | Magnetic property testing | Uniformity and low defects |
| Graphite | Thermal and electrical studies | Reduced internal porosity |
| Pharmaceutical powders | Formulation research | Controlled compaction |
| Other hard-to-form powders | Material development | Stable pressure distribution |
Caption: Typical powder materials suitable for laboratory isostatic compaction.
The process can also accommodate different mold configurations.
Thin-sheet specimens, rods, tubular samples, and other high-aspect-ratio geometries can benefit from multidirectional pressure application. The exact mold design should match the material, dimensions, pressure requirements, and intended testing method.
Why Sample Geometry Matters
Complex shapes can be difficult to compact uniformly with conventional axial pressing.
For example, a long rod-shaped specimen may experience different pressure conditions along its length. A tubular sample can present additional challenges because of its geometry and wall structure.
Isostatic pressure surrounds the mold and therefore provides a more consistent loading condition around these shapes.
This can help researchers prepare samples with fewer structural defects before sintering or characterization.
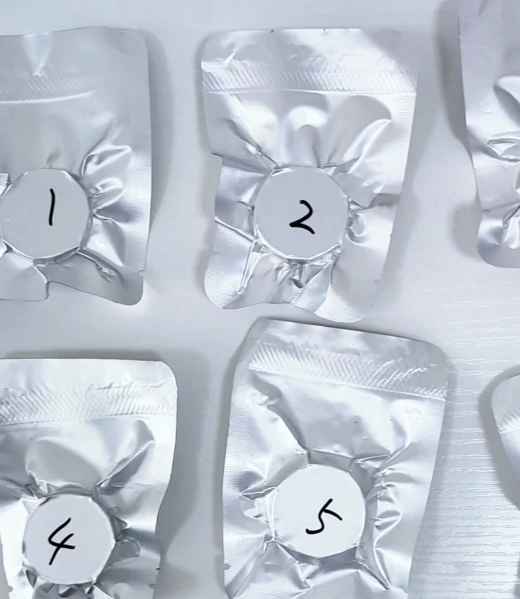
Isostatic Pressing in Materials Research
Laboratory isostatic pressing can support research workflows that require consistent powder compaction.
In university laboratories, researchers may use the equipment for ceramic processing, powder metallurgy, electrode development, and material characterization.
Corporate R&D teams can also use controlled compaction when evaluating new powder formulations or optimizing material processes.
The process is especially useful when sample quality directly affects later testing.
For example, mechanical testing requires specimens with controlled density and structure. Electrochemical testing may also require consistent electrode composition and porosity. Microstructural analysis benefits from samples with fewer forming defects.
By improving the consistency of the green body, isostatic pressing can reduce one source of variation before these later stages.
Isostatic Pressing vs. Conventional Uniaxial Pressing
The choice between pressing methods depends on the material, sample geometry, required density uniformity, production volume, and experimental objectives.
| 特徴 | 一軸プレス | 等方圧加圧 |
|---|---|---|
| Main pressure direction | One or two axial directions | Multidirectional |
| Die-wall friction | Significant factor | Greatly reduced |
| Density distribution | May vary across the compact | より均一 |
| Sample geometry | Often favors simple shapes | More flexible |
| Residual stress | 重要である可能性がある | Generally reduced |
| Automation | Depends on equipment | Programmable systems available |
| Crack and delamination risk | Depends strongly on material and process | Can be reduced through uniform pressure |
| Laboratory repeatability | Depends on operator and process control | Improved with automated cycles |
Caption: General comparison between uniaxial and isostatic powder compaction.
This comparison does not mean that isostatic pressing replaces every conventional pressing method. Uniaxial presses remain suitable for many applications.
However, when density uniformity, complex geometries, or sample integrity become critical, isostatic pressing offers important process advantages.
For applications requiring hydraulic pressure generation and controlled compaction, a hydraulic isostatic press can provide a practical equipment configuration for laboratory powder forming.
How to Select a Laboratory Isostatic Press
Selecting equipment should begin with the requirements of the actual research process.
Pressure capacity is one of the first parameters to evaluate. The required pressure depends on the powder characteristics, target density, sample dimensions, and forming method.
Researchers should also consider chamber dimensions.
The usable chamber determines the maximum mold size and the number of samples that can be processed in one cycle. A larger chamber may improve batch flexibility, while a compact chamber can suit laboratories with limited sample volumes.
Key Selection Factors
Before purchasing equipment, consider:
- Required working pressure
- Chamber dimensions
- Sample size and geometry
- Pressure medium
- 圧力制御精度
- Pressurization and pressure-release rates
- Automation level
- Mold compatibility
- Safety functions
- Data recording requirements
The control system also deserves attention.
A programmable system can help researchers establish repeatable pressure cycles. If the equipment records process data, researchers can also maintain better traceability between sample batches.
From Powder Preparation to Final Testing
Isostatic pressing should be viewed as part of a complete sample-preparation workflow.
Powder preparation, moisture control, particle size, binder content, mold filling, sealing, pressing, demolding, drying, and sintering can all affect the final result.
Even a well-controlled pressing system cannot compensate for inconsistent powder preparation.
For this reason, researchers should establish standardized procedures for each stage.
A typical workflow may include:
Powder preparation → Mold filling → Mold sealing → Isostatic pressing → Pressure release → Demolding → Drying → Sintering → Characterization
Each step should use consistent parameters where possible.
This approach allows researchers to identify the actual source of variations more effectively.
Improving Experimental Data Quality
Sample consistency has a direct relationship with experimental reliability.
If one pellet contains significantly more internal porosity than another, differences in test results may reflect sample preparation rather than the material itself.
Uniform compaction helps reduce this uncertainty.
For research teams comparing different powder formulations, controlled sample preparation can therefore improve the value of experimental comparisons.
FAQ About Laboratory Isostatic Pressing
アイソスタティックプレスは何に使用されますか?
アイソスタティックプレスは、流体圧力媒体を介して複数の方向から圧力を加えることによって粉末を圧縮する。研究所は、材料の研究とテストのために、より均一な緑体を生成するためにそれを使用しています。
アイソスタティックプレスはペレットの割れを減らすことができますか?
それは、不均一な圧力分布、密度勾配、および残留応力に関連するひび割れリスクを大幅に低減することができる。実際の結果は、粉末の特性とプロセスパラメータによって異なります。
実験室のアイソスタティックプレスではどのような粉末を加工できますか?
用途としては、高度なセラミックス、金属粉末、電極材料、磁性材料、グラファイト、医薬品粉末、および制御された粉末圧縮を必要とする他の材料を挙げることができる。
アイソスタティックプレスは複雑なサンプル形状に適していますか?
はい。柔軟な金型により、研究者はさまざまなジオメトリを作成できます。金型設計は、必要なサンプル形状と加工条件に一致する必要があります。
自動制御は再現性を向上させますか?
自動制御は、一貫した加圧、保圧、および圧力放出サイクルを維持することにより、再現性を向上させることができます。手作業によるバラツキも軽減します。
研究者は購入する前に何を考慮すべきですか?
圧力範囲、チャンバーサイズ、サンプル形状、自動化、圧力制御精度、金型適合性、安全機能、およびデータ記録要件をすべて評価する必要があります。
結論
Cracking, delamination, uneven density, and residual stress can create significant problems during powder compaction. Conventional uniaxial pressing can contribute to these defects because pressure and die-wall friction may produce non-uniform stress and density distributions.
Laboratory automatic isostatic pressing provides a different approach. By using a fluid pressure medium to apply pressure around a flexible mold, the process promotes more uniform powder compaction. Automated pressure control further improves process consistency and experimental repeatability.
For materials laboratories working with ceramics, metal powders, electrode materials, graphite, magnetic materials, or other demanding powders, isostatic pressing can improve the quality and consistency of green bodies before sintering and testing. The correct equipment configuration should ultimately match the powder characteristics, sample geometry, pressure requirements, and research workflow.